The evidence behind every claim.
No machines, no electricity, no production waste. Certified B Corporation, aligned to nine UN Sustainable Development Goals. This page states what we can prove and what we are still working on.
What a factory electrifies, and what we do by hand.
A conventional knitwear factory draws electricity at five stages. KOCO uses none of them. Below, each stage a factory powers is set against how the same work is done by hand, with the same bamboo and timber needles from first stitch to last.
This is not a carbon-offset story. There is no machine to switch off because there was never a machine to switch on.
- Knitting
- Conventional factoryPowered flat-bed and circular knitting machines draw continuous grid electricity to form fabric at speed.
- KOCOEach garment is knitted by hand on bamboo and timber needles by a single named artisan. No motor, no loom, no current.
- Joining
- Conventional factoryLinking and seaming machines run on mains power to join panels in continuous runs.
- KOCOPanels are joined by hand, stitch by stitch, with the same needles used to knit them.
- Finishing
- Conventional factorySteam presses and heated finishing tables draw electricity to set shape and close seams.
- KOCOSeams are closed and threads finished by hand. No steam press, no heated table, no power tool.
- Blocking
- Conventional factoryPowered steam boilers and electric blocking boards set the garment to its final dimensions.
- KOCOGarments are blocked by hand on flat boards, shaped to measurement, and left to settle in ambient air.
- Washing
- Conventional factoryIndustrial washing machines and centrifugal extractors run on electricity to clean and finish fabric.
- KOCOEach garment is washed by hand in cool water and laid flat to dry. No machine, no spin cycle.
Nine goals, each tied to something specific we do.
We list the goal and the reason it applies. No badges, no icons, no decoration. The connection is the content.
- 01Goal 1 – No Poverty: paid work that did not previously exist for women in these villages.
- 02Goal 4 – Quality Education: literacy and basic maths taught so artisans can read written patterns.
- 03Goal 5 – Gender Equality: a workforce of women trained into skilled, paid, named work.
- 04Goal 8 – Decent Work and Economic Growth: fair wages and a seven-month paid apprenticeship.
- 05Goal 9 – Industry, Innovation and Infrastructure: a written-pattern method with no industry precedent.
- 06Goal 10 – Reduced Inequalities: women who had never been to school enter skilled trade.
- 07Goal 11 – Sustainable Cities and Communities: work concentrated in village hubs, not urban factories.
- 08Goal 12 – Responsible Consumption and Production: zero electricity and no production waste.
- 09Goal 13 – Climate Action: a production process with no energy input beyond the artisan's hand.
The fibre we specify, and where its impact actually sits.
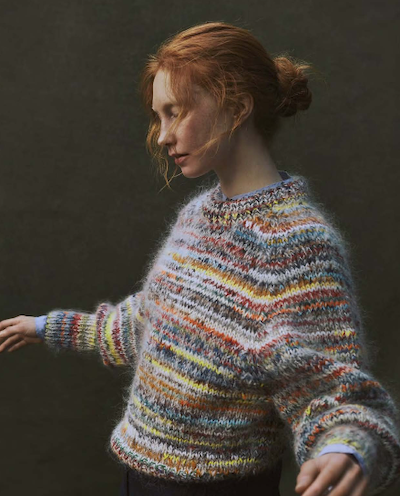
We source natural fibres including Australian merino, mohair, silk and organic cotton, and work with spinners and dyers on custom developments. The KOCO Mohair Jumper is 70% mohair, 30% silk.
We are precise about the boundary of our claim. Zero electricity covers KOCO production. Spinning and dyeing are carried out by third-party mills and carry their own energy and water loads. We trace those mills on request and prefer lower-impact options where a brief allows, but we do not fold them into a claim we cannot stand behind.
Hubs, not homes. Trained, not handed a deadline.
Artisans work from centralised village hubs across four villages: Temple Village, Farmer Village, Lentil Village and Bus Village. They do not work from home. The hub model is how we hold quality, fair conditions and a shared standard.
Most artisans had never been to school. Each enters through a seven-month paid apprenticeship in which they are taught English literacy and basic maths, so they can read written knitting patterns rather than work from sketches. Hundreds of women artisans have been trained this way.
Every garment carries a swing tag naming the artisan who made it. Traceability is not a label added afterwards; it is the structure of how the work is organised.
A sustainability page with no limits reads as greenwashing.
We state these plainly. They are the gaps a compliance lead will find anyway, and naming them is part of the evidence.
- Yarn spinning and dyeing sit outside our production and carry energy and water loads we do not control. We are working to map and prefer lower-impact suppliers for the fibres we specify most often.
- Freight to brand warehouses is air or sea and is not zero-carbon. We consolidate shipments where lead times allow and are honest about the gap between hand production and global logistics.
- We do not yet hold a published figure for artisan workforce numbers or a third-party living-wage audit. We state the qualitative position rather than an unverified number, and are working toward verified reporting.
- Our written-pattern method is labour-intensive by design. That is the basis of quality and inclusion, but it sets a lead time a machine factory will always beat. We are improving pattern throughput without compromising the method.
Answered directly.
The claim is structural rather than a meter reading: there is no machinery on site to power. Production is hand-knitting, hand-joining, hand-finishing, hand-blocking and hand-washing. B Corp assessment reviews the operating model. We welcome a brand-side audit and will walk a compliance lead through any hub on request.
Through trained artisan numbers, not through machine speed. Production scales from a single piece to 1000 or more by adding trained knitters and written patterns, one per size. Consistency comes from the written pattern and the individual tension swatch knitted before each garment, not from a machine setting.
The B Corp certification, the written-pattern methodology, the swing tag that names the artisan who made each garment, and site access to the village hubs. Where a specific certification or figure is requested that we do not hold, we say so rather than supply an unverified number.
No, and we do not claim it does. The zero-electricity claim covers KOCO production: knitting, joining, finishing, blocking and washing. Yarn spinning, dyeing and freight are handled by third parties and carry their own energy profiles, which we can trace on request.
Artisans work from centralised village hubs, not from home, and are trained through a seven-month paid apprenticeship. They are not gig workers handed a pattern and a deadline. The hub model is part of how quality and fair conditions are held.
Want the evidence pack for your compliance file?
Send your tech pack or your sustainability questionnaire. We will come back with feasibility, the evidence behind each claim, and what we can and cannot yet verify.